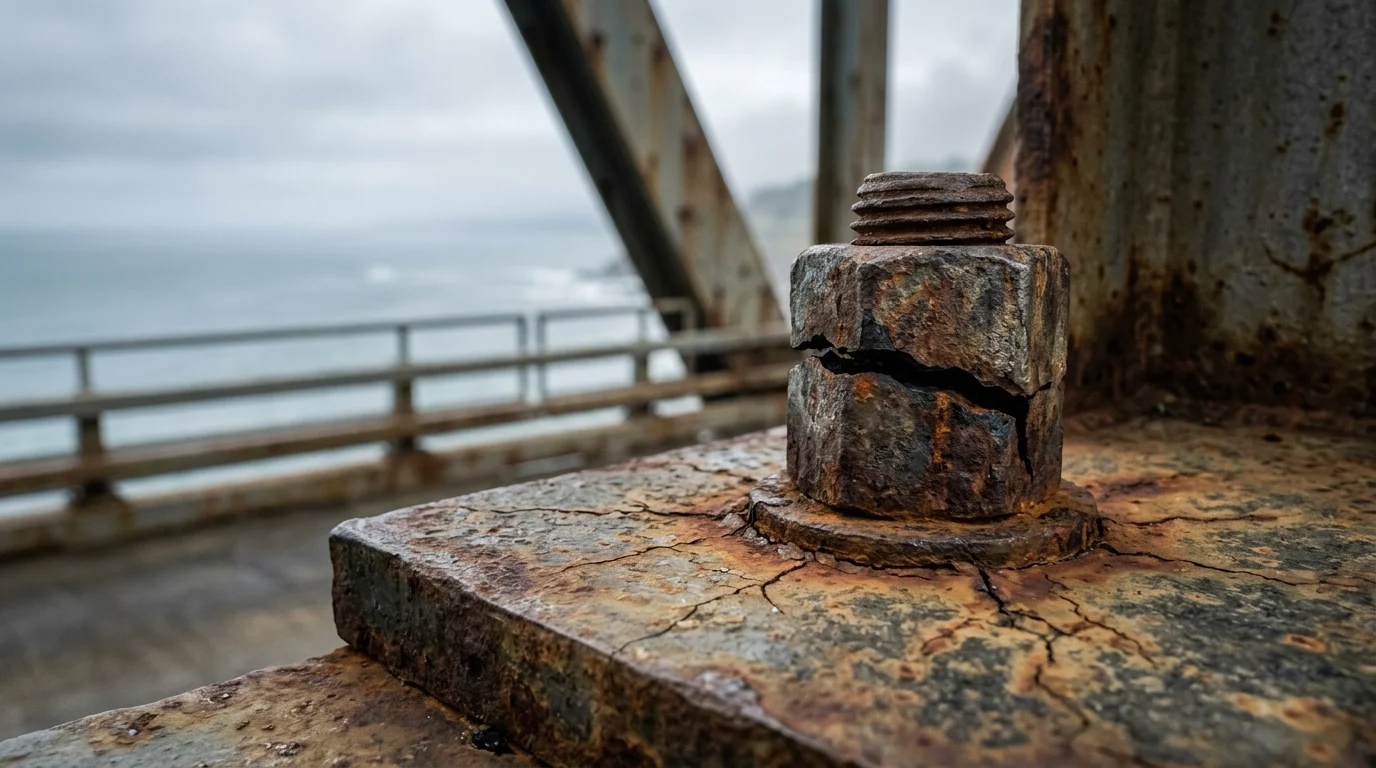
The Bridge Bolt Failure Case: A Costly Lesson
A cross-sea bridge in a coastal city experienced batch fracture of M30 bolts (bridge bolt selection) at the bridge deck connections only 3 years after opening. The direct repair costs were substantial, and the indirect losses from logistics detours and construction delays due to closure were even greater. The accident exposed 5 gaps in the selection logic, from working condition assessment to supplier verification. As Chief Engineer of Yaxiio, I have deconstructed this selection logic, with standard numbers and checkpoints for each step. By the end you will know how to select bolts for corrosive marine environments and be able to audit suppliers and inspect incoming bolts to prevent stress corrosion cracking.
Step 1: Working Condition Assessment: Not All Bridges Need “Typhoon-Resistant” Bolts
Core Issue: Where is the intersection of corrosive environment and mechanical load?
The most typical mistake: inland bridges copying the cross-sea bridge solution, tripling costs; cross-sea bridges using ordinary galvanized bolts, leading to stress corrosion cracking within 3 years. Working condition assessment must quantify 3 parameters:
- Corrosion Category: According to ISO 9223, from C1 (dry interior) to CX (extreme marine). The bridge tower area of a cross-sea bridge falls under C5-M (high marine corrosion), and the area below the deck falls under C4 (high industrial corrosion). Simply writing “coastal” is not specific.
- Stress State: Bridge connections bear alternating stress + continuous preload. According to ISO 898-1, the fatigue limit of grade 8.8 bolts is only about 80 MPa, while grade 12.9 can reach 120 MPa. The latter must be selected for typhoon zones.
- Temperature and Humidity: After asphalt pavement on the bridge deck, the working temperature of bolts can reach 60-80°C, accelerating the failure of the galvanized coating. In this case, the lifespan of Solution A’s grade 8.8 hot-dip galvanized bolt assemblies (M16-M24) is directly halved.
Checkpoints:
- [ ] Is the corrosion category marked according to ISO 9223?
- [ ] Is the fatigue life calculated according to ISO 898-1?
- [ ] Have the extreme bridge deck temperatures been measured?
Step 2: Standard Comparison: GB/T 3098.1-2010 and ISO 3506 Are Not “Roughly the Same”
Core Issue: Can national, American, and European standards be mixed?
A high-speed rail bridge accident occurred when the construction team replaced ISO 3506 A4-80 stainless steel bolts with GB/T 3098.1-2010 grade 10.9 bolts. The result was hydrogen embrittlement fracture. The reason: the hydrogen embrittlement sensitivity of carbon steel bolts (per ISO 15330) is completely different from that of stainless steel, and the hydrogen embrittlement risk of the coating process (Dacromet vs. zinc plated) differs significantly.
Standard Comparison Table:
| Parameter | Solution A · Economy | Solution B · Standard | Solution C · Premium |
|---|---|---|---|
| Strength Standard | GB/T 3098.1-2010 | GB/T 3098.1-2010 | ISO 898-1:2013 |
| Corrosion Standard | GB/T 5267.1-2002 | ISO 9227:2017 | ISO 12944-9:2018 |
| Hydrogen Embrittlement Test | No Requirement | ISO 15330:2018 | ISO 15330:2018 |
| Fatigue Test | No Requirement | GB/T 13682-1992 | ISO 3800:2019 |
Key Point: Solution C’s 2205 duplex stainless steel bolts (M24-M36) must be tested for hydrogen embrittlement according to grade 12.9 of ISO 898-1, because duplex stainless steel may precipitate sigma phase at high temperatures (e.g., during bridge deck asphalt construction), leading to brittleness. This is often missed in many factory inspection reports.
Checkpoints:
- [ ] Does the bolt standard match the corrosion category?
- [ ] Is the supplier required to provide a hydrogen embrittlement test report (ISO 15330)?
- [ ] Do duplex stainless steel bolts have sigma phase testing (ASTM A923)?
Step 3: Material Confirmation: 316L Stainless Steel Is Not a “Universal Anti-Corrosion” Solution
Core Issue: Who decides the combination of material grade and coating?
A cross-sea bridge used 316L stainless steel bolts (Solution B Standard), and pitting corrosion appeared at the bridge deck expansion joints after 3 years. The reason: In a chlorine-containing environment (seawater splash + bridge deck heat radiation) above 60°C, the Pitting Resistance Equivalent Number (PREN) of 316L is only 24-26, while 2205 duplex stainless steel (Solution C Premium) has a PREN ≥ 35.
Material Selection Logic:
- Low Corrosion (C2-C3): Solution A’s 304 stainless steel bolts (M12-M20) or grade 8.8 hot-dip galvanized bolts (M16-M24) are sufficient.
- Medium Corrosion (C4): Solution B’s 316L stainless steel bolts (M16-M24) or Dacromet coated bolts (M20-M30). Note: Dacromet coating (per ISO 10683) has a temperature resistance ≤ 250°C, which is fine for bridge deck asphalt construction (160°C), but cannot be used in welding areas.
- High Corrosion (C5-CX): Solution C’s 2205 duplex stainless steel bolts (M24-M36) or grade 12.9 ultra-high strength bolts (M30-M42) + PTFE coating. PTFE coating (per ASTM D4894) can reduce the friction coefficient to 0.08-0.12, preventing preload loss.
Checkpoints:
- [ ] Is the stainless steel grade selected based on PREN value?
- [ ] Does the coating temperature resistance cover the construction temperature?
- [ ] Is the supplier required to provide a chemical composition report (per ASTM E1086)?
Step 4: Supplier Audit: Heat Treatment Furnace and Hydrogen Embrittlement Test Equipment Are Both Essential
Core Issue: Heat treatment furnace and hydrogen embrittlement test equipment are both essential
A supplier was found to have used a regular electric furnace instead of a controlled atmosphere furnace for heat treatment, resulting in large hardness dispersion of bolts. More subtly, the hydrogen embrittlement test equipment was a decoration and had never been calibrated.
Supplier Audit Checklist:
| Inspection Item | Standard Requirement | Solution A Supplier | Solution B Supplier | Solution C Supplier |
|---|---|---|---|---|
| Heat Treatment Furnace | Controlled atmosphere furnace + temperature recording | Optional | Required | Required |
| Hydrogen Embrittlement Test | ISO 15330 equipment + calibration records | Not required | Required | Required |
| Torque Coefficient Test | GB/T 1231-2024 | Optional | Required | Required |
| Salt Spray Test Chamber | ISO 9227 + 72h continuous operation | Optional | Required | Required |
| Batch Traceability System | Each batch has unique number + composition report | Optional | Required | Required |
Key Point: Solution C’s anti-loosening self-locking bolts (M16-M30) must be tested on-site for vibration loosening (per ISO 16130) during factory audit. Many suppliers’ “anti-loosening” is just adding a nylon ring, and the torque loss after vibration is significant.
Checkpoints:
- [ ] Does the heat treatment furnace have a temperature recorder?
- [ ] Does the hydrogen embrittlement test equipment have a third-party calibration certificate?
- [ ] Is the torque coefficient test demonstrated on-site?
Step 5: Incoming Inspection: Hardness, Coating Thickness, and Thread Accuracy Are All Essential
Core Issue: Hardness, coating thickness, and thread accuracy are all essential
In one project, the incoming bolts had no rust on appearance, but the torque could not be reached during installation. The reason: the thread accuracy was not up to standard (6g grade actually achieved 6h), resulting in excessive friction coefficient. More seriously, the coating thickness was uneven, with local areas below the standard requirement.
Incoming Inspection Checklist:
| Inspection Item | Standard | Sampling Ratio | Nonconformity Handling |
|---|---|---|---|
| Hardness | GB/T 3098.1 | 5% per batch | Reject entire batch |
| Coating Thickness | ISO 2178 | 3% per batch | Local repair or reject |
| Thread Accuracy | GB/T 197-2003 | 2% per batch | Reject entire batch |
| Torque Coefficient | GB/T 1231-2024 | 1% per batch | Adjust installation process or reject |
| Hydrogen Embrittlement Test | ISO 15330 | 1 group per batch | Reject entire batch |
Key Point: Solution C’s anchor anti-corrosion grease (poured type/paraffin-based) must be tested on-site for dropping point (per GB/T 4929-1985). Many projects skip this test, resulting in grease failure at high temperatures and loss of protection.
Checkpoints:
- [ ] Is the hardness test performed according to GB/T 3098.1?
- [ ] Is the coating thickness measured according to ISO 2178?
- [ ] Is the thread accuracy checked according to GB/T 197-2003?
Summary: Two Key Decision Points
- For high corrosion marine environments (C5-CX), 2205 duplex stainless steel bolts with PREN ≥ 35 are preferred over 316L stainless steel, which has a PREN of only 24-26.
- Supplier audits must verify the presence of a controlled atmosphere heat treatment furnace and calibrated hydrogen embrittlement test equipment; otherwise, the risk of hydrogen embrittlement and inconsistent hardness is high.
Next Steps: Prepare These Before You Procure
- [ ] Define the corrosion category of your bridge location according to ISO 9223 (C1 to CX).
- [ ] Calculate the required fatigue limit based on the stress state and select the appropriate bolt grade per ISO 898-1.
- [ ] Prepare a supplier audit checklist including heat treatment furnace, hydrogen embrittlement test equipment, and torque coefficient test.
- [ ] Plan incoming inspection items: hardness, coating thickness, thread accuracy, and hydrogen embrittlement test, with sampling ratios and nonconformity handling procedures.
Deep Reading
More systematic selection, procurement, or inspection guides.
- Fastener Selection for Agricultural Processing Equipment: From Failure Mechanisms to Acceptance Decisionwhitepaper
A more systematic guide on a related selection or inspection topic.
- Livestock Facility Fastener Selection: Corrosion Zones, Materials, and Inspectionwhitepaper
A more systematic guide on a related selection or inspection topic.
- Corrosion-Resistant Fastener Selection for Municipal Water Treatment Plantswhitepaper
A more systematic guide on a related selection or inspection topic.
This article helps with selection and application. But in real projects, specifying the right part is only step one, finding the right factory, controlling quality, and delivering on time is the real challenge. We cover fasteners, rubber, plastics, and industrial textiles across four categories, from Zhejiang industrial clusters to your project site, one team, end to end.
See Our Supply Chain Capabilities →